Sialkot factory · MOQ from 50 units · Samples in 7–10 days
- BSCI audited & ISO 9001
- [email protected]
- Mon–Sat, 09:00–18:00 (PKT)
Precision-engineered for professional matches, club practice, indoor academies, and commercial bowling machines. Manufactured under ISO 9001 and BSCI compliance.
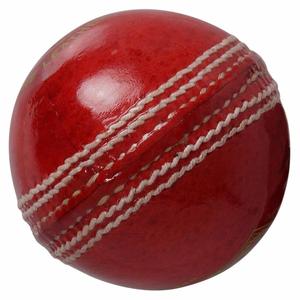
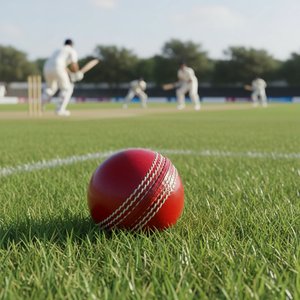
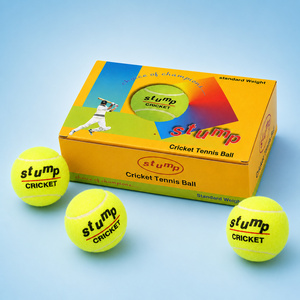
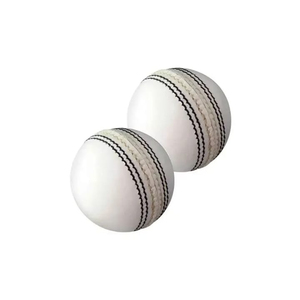
In professional cricket, the performance of a cricket ball is defined by physics, chemistry, and precise manual craftsmanship. As an established OEM/ODM manufacturing facility based in Sialkot, Pakistan—the world's historic capital for hand-stitched sporting goods—we maintain rigorous material selection and dimensional controls to ensure compliance with the Marylebone Cricket Club (MCC) Laws of Cricket (Law 4) and International Cricket Council (ICC) tournament specifications.
A elite-level match ball requires an exact balance of resilience, seam height, hardness retention, and moisture resistance. Below is a deep breakdown of the critical core components engineered within our facility:
Our match-grade balls feature a 100% natural, high-density granulated cork core wrapped tightly with premium worsted wool yarn. Unlike cheap synthetic rubber cores, our layered cork construction guarantees consistent bounce height (between 120cm–135cm off hard surfaces) and maintains structural integrity across 80+ overs of high-impact play.
We source premium top-grain cowhide and steerhide, subjected to traditional alum-tanning or chrome-tanning processes. Alum tanning preserves the natural fibrous strength of the hide, yielding a rich red, white, or pink finish that accepts traditional wax polishes without cracking or deteriorating under damp pitch conditions.
The defining characteristic of an elite cricket ball is its prominent seam. Master craftsmen stitch 54 to 80 internal stitches alongside 6 prominent external rows of wax-coated linen thread. This elevated seam profile grants seam bowlers maximum lateral movement (seam deviation) and enhanced swing mechanics through aerodynamic boundary-layer manipulation.
To assist global procurement officers, sports brand buyers, and academy distributors in choosing the optimal product line for their target market, we have compiled a definitive technical specification breakdown across all manufacturing lines:
| Ball Category | Shell Material | Core Composition | Weight & Size Specs | Primary Application | Expected Lifespan |
|---|---|---|---|---|---|
| Professional Match | Alum-Tanned Top Grain Leather | 5-Ply Cork & Wool Worsted Core | 155.9g – 163g / 224mm–229mm | Multi-day Test & 50-Over Matches | 80+ Overs High Resilience |
| Club & League Match | Chrome-Tanned Bovine Leather | 3-Ply Cork Matrix / Rubber Blend | 156g Standard (Custom Youth 142g) | Regional Leagues & Club Tournaments | 40 – 60 Overs Play |
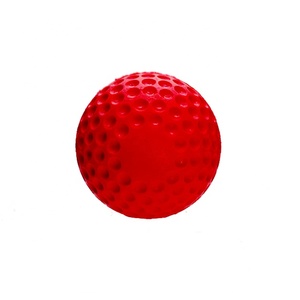
| Dimpled Machine Ball | Micro-Cellular Polyurethane (PU) | Hollow / Density-Engineered PU | 9-Inch / 140g – 150g Weight | Automated Bowling Machines & Nets | 5,000+ Machine Deliveries |
| Indoor Soft / PVC | Flexible Polyvinyl Chloride (PVC) | Soft Foam / Hollow Air Core | 70mm Diameter / 80g – 90g | Indoor Academies & School Training | All-Weather / Multi-Season |
| Heavy Tennis Training | High-Grade Felt / Vulcanized Rubber | Solid High-Density Rubber Core | 70mm Diameter / 85g – 125g | Street Cricket, Drills & Wet Conditions | Extremely Durable (Non-Burst) |
The global sports equipment market is undergoing rapid evolution driven by technological integration, environmental sustainability regulations, and shifting player demographics. For international brand owners, retail chains, and sports federation importers, staying ahead of manufacturing trends is crucial for maintaining market share and healthy profit margins.
Importers across the UK, European Union (EU), Australia, and North America are increasingly subjected to strict chemical usage audits. Traditional leather processing often relied on heavy metals and azo dyes. Our factory leads the transition toward eco-friendly vegetable tanning, chrome-free dye formulations, and non-toxic wax finishes fully compliant with EU REACH regulations and UKCA standards.
Moisture absorption is the leading cause of leather degradation and weight inflation during damp day-night matches or wet outfield play. Future procurement requests are heavily shifting toward nanotechnology-based hydrophobic leather sealants. These invisible nano-coatings prevent water ingress while allowing the leather to breathe, keeping the ball within legal weight limits for longer durations.
With data analytics reshaping coaching and broadcasting, OEM manufacturing is expanding to include micro-sensor integration. Next-generation ODM projects incorporate ultra-lightweight inertial measurement units (IMUs) embedded directly into the central cork core, recording real-time spin rate (RPM), velocity, seam orientation, and launch angle without altering balance or weight dynamics.
Rooted in Sialkot, Pakistan—a world-renowned hub producing high-performance athletic equipment for global brands—our facility bridges traditional artisan craft with modern quality assurance protocols.
Eliminate third-party trading markups. We handle every step under one roof: hide cutting, core formation, hand stitching, logo debossing, lacquering, and final packaging. This guarantees transparent pricing and direct technical communication with our engineering supervisors.
Our modern workshop operates under strict ISO 9001 Quality Management Systems and BSCI social compliance standards. We guarantee fair labor practices, safe working conditions, clean environmental controls, and full traceability across every shipment batch.
We empower growing sports brands, academies, and regional clubs. While traditional factories demand thousands of units, our flexible line arrangements accommodate starting orders from just 50 units, backed by pre-production physical samples delivered in 7–10 days.
Essential answers regarding order MOQs, customization possibilities, production timelines, international shipping, and quality assurance protocols.
Our standard stock specifications start at an industry-leading low threshold of 50 units per line. For fully customized private-label programs featuring bespoke logo gold-foil stamping, unique colorway leather dyeing, and custom barcoded retail boxes, our standard starting MOQ is 100 units per specification.
Physical pre-production samples with custom logo branding are manufactured, inspected, and shipped via express courier within 7 to 10 working days. Mass production runs typically take 25 to 35 days, depending on batch quantity and leather tanning schedules. A dated production roadmap is issued with every formal quotation.
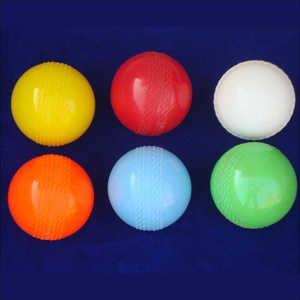
Yes. We produce traditional cherry red balls for daytime multi-day games, high-visibility white balls for limited-overs white-ball cricket under floodlights, and modern pink balls for day-night Test matches. Custom training colors (yellow, neon green, two-tone split colors for swing analysis) are readily available upon request.
Every batch undergoes strict AQL 2.5 final inspection. Testing protocols include ring-gauge dimensional checks (ensuring 224mm-229mm circumference), weight verification (155.9g-163g), drop-bounce height evaluation, seam height measurement, and compression hardness testing prior to export packing.
We provide flexible commercial terms based on your logistics preference: EXW, FOB (Karachi Port), CIF, and DDP (Delivered Duty Paid directly to your warehouse). Standard payment terms are 30% advance deposit by T/T upon proforma approval, with the remaining 70% balance payable against shipping documentation (Bill of Lading).
Absolutely. We offer complete OEM branding solutions including metallic gold/silver foil stamp printing on the leather, customized inner tissue wrap, branded individual rigid display boxes, barcoded polybags, and heavy-duty 5-ply export master cartons ready for direct retail distribution.
Looking to launch your private label cricket line, stock your academy network, or source high-performance match balls directly from Sialkot's top craftsmen? Connect directly with our export engineering team for instant technical consultation and pricing breakdown.
Inquire Now