Sialkot factory · MOQ from 50 units · Samples in 7–10 days
- BSCI audited & ISO 9001
- [email protected]
- Mon–Sat, 09:00–18:00 (PKT)
Engineered for professional sports clubs, athletic brands, collegiate leagues, and international distributors.
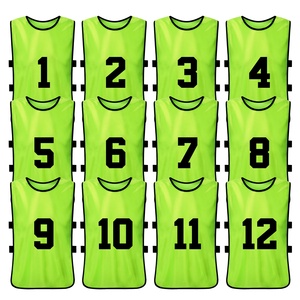
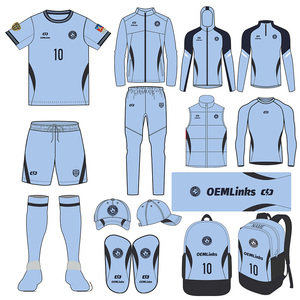
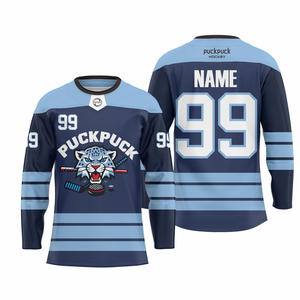
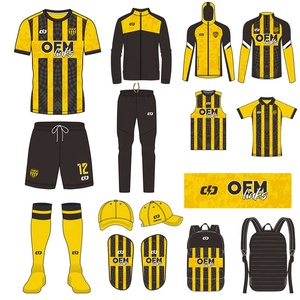
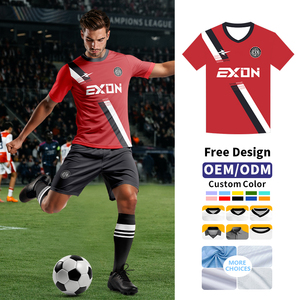
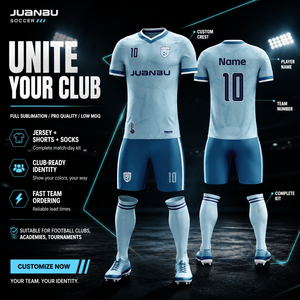
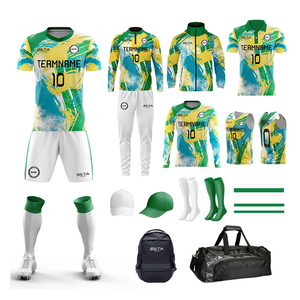
The global athletic apparel market is experiencing a profound structural shift driven by modern consumer demand for hyper-customization, eco-friendly textile performance, and ultra-short lead times. As premier China wholesale team apparel suppliers and exporters, our manufacturing infrastructure bridges high-capacity synthetic textile mills with advanced cut-and-sew technology to deliver professional-grade uniforms to global markets.
Historically, commercial teamwear procurement required brand managers to choose between low-cost volume manufacturing or flexible micro-customization. Today, through vertical integration—encompassing automated pattern plotting, high-density digital dye-sublimation, and ISO-certified in-line quality assurance—our facility eliminates supply chain trade-offs. Procurement directors gain access to factory-direct bulk pricing alongside agile OEM order terms (MOQ starting at 50 units for specialized lines).
Utilizing high-precision Italian KIAN sublimation inks and Japanese Mimaki digital printers, we guarantee color fastness rating 4.5+ (ISO 105 standard) without blocking thermal breathability.
Our production facilities maintain active BSCI social compliance audits, ISO 9001 quality system certifications, and OEKO-TEX Standard 100 fabric safety guarantees for global customs clearing.
Engineered for high-tempo sporting seasons: pre-production digital CAD mockups within 24 hours, physical samples delivered globally in 7 to 10 working days.
Elite athletic performance requires deliberate textile composition. Modern team apparel cannot rely on off-the-shelf basic fabrics; it demands multi-component yarn structures targeted to specific sports movement vectors:
As search intent analysis demonstrates, institutional sportswear buyers are actively shifting away from single-season disposable uniforms toward sustainable, technologically integrated supply chains. Forward-looking procurement directors should align with manufacturers investing in the following critical developments:
Environmental governance (ESG) compliance has moved from a branding luxury to a mandatory vendor criterion across Europe and North America. Leading Chinese exporters are migrating primary jersey lines to recycled post-consumer polyethylene terephthalate (rPET) yarns derived from ocean-bound plastics. These circular textiles achieve identical tensile strength, color vibrancy, and moisture-wicking characteristics as virgin synthetic polymers while cutting carbon footprints by up to 45% per unit.
Traditional warehousing of static inventory risks capital lockup and stock obsolescence. The future of athletic teamwear lies in agile digital manufacturing. By establishing modular pattern cutting and digital sublimation units, suppliers enable sports brands and regional distributors to launch custom capsule collections with low initial capital expenditure, ordering only what end-users consume.
Post-athletic hygiene engineering now incorporates permanent silver-ion or natural zinc-based anti-microbial treatments applied directly to yarn extrusions during fabric milling. This inhibits odor-causing bacteria build-up over repeated match cycles, significantly extending garment service life for school districts, university athletic departments, and commercial fitness chains.
Partner directly with an audited Chinese team apparel exporter. Request technical spec sheets, fabric swatches, or a custom B2B quotation from our engineering team today.
Inquire Now