Sialkot factory · MOQ from 50 units · Samples in 7–10 days
- BSCI audited & ISO 9001
- [email protected]
- Mon–Sat, 09:00–18:00 (PKT)
Precision-engineered martial arts protectors, ergonomic guards, and certified lifting equipment manufactured for worldwide OEM brands and commercial gym suppliers.
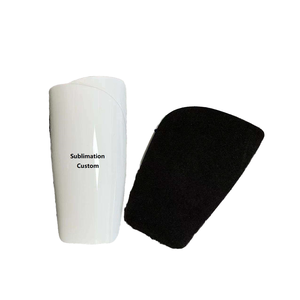
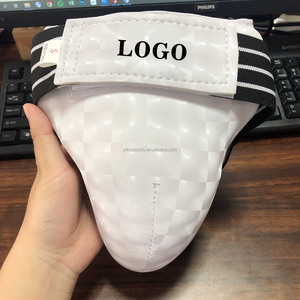
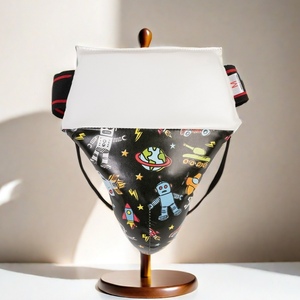
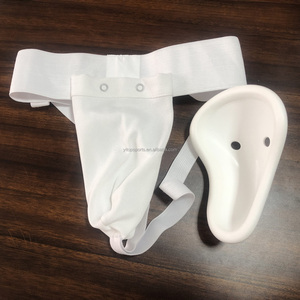
Navigating European Personal Protective Equipment (PPE) Directives, Tensile Load Dynamics, and Leather/Nylon Material Engineering for B2B Importers.
In global fitness equipment procurement, securing a CE Certified Lifting Belt Manufacturer & Factory is no longer merely a branding preference—it is a mandatory risk-mitigation benchmark for EU, UK, and North American distributors. Personal protective accessories used during max-load strength training, powerlifting, and combat conditioning fall under rigorous structural safety metrics. Under European Regulation (EU) 2016/425 (Personal Protective Equipment), body support devices designed to prevent physical harm during high-load spinal compression must verify both mechanical integrity and non-toxic chemical composition.
When heavy athletes execute heavy compound movements such as deadlifts, squats, or overhead presses, intra-abdominal pressure (IAP) increases drastically. A compliant lifting belt serves as a rigid biomechanical wall against which the abdomen expands. This stabilization drastically reduces shear forces on the lumbar spine (specifically L4-L5 and L5-S1 vertebrae). If a belt's leather shear strength or buckle locking mechanism fails under a 300 kg stress load, the potential for catastrophic athlete injury is severe. Consequently, tier-1 wholesale importers require documented proof of tensile stress testing exceeding 15,000 N, fatigue resistance, and non-hazardous tanning processes (REACH compliance).
Our engineered 10mm and 13mm leather powerlifting belts deliver constant intra-abdominal pressure stabilization. Custom contoured cutouts minimize friction against the ribs and hip crest while preserving maximal posterior structural rigidity.
Equipped with zinc-plated cast steel lever mechanisms and heavy-gauge stainless steel prongs. Tested against repeated torque stress without micro-fracturing or slippage during max-effort lifts.
Fully compliant with ISO 9001:2015 Quality Management Protocols, BSCI Social Compliance Audits, and chemical testing for azo dyes, phthalates, and chromium-6 content.
A definitive technical breakdown of leather hide selection, synthetic core laminated composites, and stitch-line density for industrial fitness product development.
| Belt Architecture / Material | Tensile Load Rating | Structural Stiffness Index | Target Fitness Application | Core OEM Customization Options |
|---|---|---|---|---|
| Full-Grain Cowhide Leather (10mm - 13mm) | 18,500 N+ | Maximum (Rigid) | Competitive Powerlifting, IPF Spec | Debossed Logos, Suede Lining, Steel Levers |
| High-Density Microfiber Leather | 14,000 N | Medium-High | Commercial Gym Gear, Bodybuilding | Screen-printed graphics, Custom Colorways |
| 1000D Cordura Nylon with EVA Core | 9,500 N | Flexible Ergonomic | Functional Fitness, Cross-Training, Olympic Weightlifting | Quick-Release Ratchet Buckles, Velcro Patches |
| Dipping Belts (Reinforced Chain / Neoprene) | 12,000 N (Chain Load) | Contoured Flex | Weighted Calisthenics & Bodyweight Additions | Heavy-Duty Carabiners, Thick Neoprene Padding |
A critical point of failure in low-grade lifting belts lies in structural seam degradation. At our Sialkot factory, every lifting belt and protective groin/shin guard utilizes Bonded Nylon 138 heavy-duty thread with a stitch density precisely calibrated between 6 to 8 stitches per inch (SPI). Dual lock-stitching prevents unraveling even if an outer loop is exposed to heavy barbell knurling friction. Furthermore, leather edges undergo automated beveling, burnishing, and sealed organic edge-kote finishing to resist sweat absorption and prevent material delamination over long-term commercial usage.
Key innovations driving B2B manufacturing growth, eco-friendly tanning, smart ergonomic integration, and hyper-customized private labeling.
Global brands are shifting away from traditional chromium-tanning due to stringent European environmental policies. Future procurement heavily favors eco-friendly vegetable-tanned hides that utilize natural plant tannins. This process yields a denser fiber structure, eliminates skin-allergen risks, and aligns with corporate ESG (Environmental, Social, and Governance) scorecards.
Traditional two-prong steel buckles are increasingly being replaced by adjustable micro-ratchet and quick-release lever systems. Made from zinc alloy or lightweight aircraft-grade aluminum, these systems allow athletes to change belt tightness by micro-increments between heavy sets without tools, elevating consumer demand across commercial retail channels.
Direct factory execution without trading middlemen—combining historic sports gear craft with modern ISO quality assurance protocols.
From raw hide selection, precision die-cutting, EVA foam heat moulding, and CNC embroidery to automated packing. Every step is monitored under one roof to maintain total cost control and strict quality standards.
We support emerging fitness brands and established gym chains alike. Stock specification orders start at MOQ 50 units, with pre-production physical samples crafted and dispatched within 7–10 working days.
Complete custom branding: laser-etched metal buckles, debossed leather logos, woven brand patches, custom barcode polybags, and retail packaging built strictly to your technical dossier.
Clear, definitive technical answers regarding OEM custom orders, CE documentation, quality control, and international logistics.
For standard OEM production runs using stock leather colors or high-density microfiber, our baseline Minimum Order Quantity (MOQ) is 50 units per design/colorway. For custom custom-dyed leather, specialized hardware plating, or full private-label custom retail boxes, the standard starting threshold is 100 units. We offer flexible size-breakdown mixing (e.g., Small to XXL) within a single order batch.
Physical pre-production samples—complete with your custom brand logo, stitching specifications, and selected lever mechanism—are produced and shipped via express courier within 7 to 10 working days following vector artwork confirmation. Mass production timelines typically range between 25 to 35 business days depending on total container order volume and leather tanning schedules.
Our manufacturing workflow enforces strict AQL 2.5 (Acceptable Quality Limit) standards. Every batch of lifting belts and martial arts groin/shin guards is evaluated for tensile shear strength, seam tear resistance, buckle torque thresholds, and chemical non-toxicity (zero azo dyes, REACH compliance, low chromium content). Full laboratory test documentation and material certificate of analysis (COA) are supplied prior to shipment dispatch.
Yes. We manufacture powerlifting belts matching exact IPF dimensions: maximum 10cm (4 inches) belt width, maximum 13mm thickness, with approved buckle and lever mechanism tolerances. Our engineering team builds to match competition standards for powerlifting federations globally.
We offer standard commercial Incoterms including EXW, FOB Karachi, CIF, and DDP (Delivered Duty Paid) directly to your distribution center in the US, Europe, UK, Canada, or Australia. Standard commercial payment terms are 30% advance deposit via T/T upon order confirmation and 70% balance payment upon presentation of the final inspection report and Copy Bill of Lading (B/L), or Irrevocable L/C at sight for large container volumes.
Send us your technical specification sheet, logo vector files, or product requirements. Our factory engineering team will reply with a detailed costed quote within 24 business hours.